
Semi-Automatic Perfume Bottle Collar Pressing Machine for Perfume, Cologne, Body Mist and Essential Oil Bottles
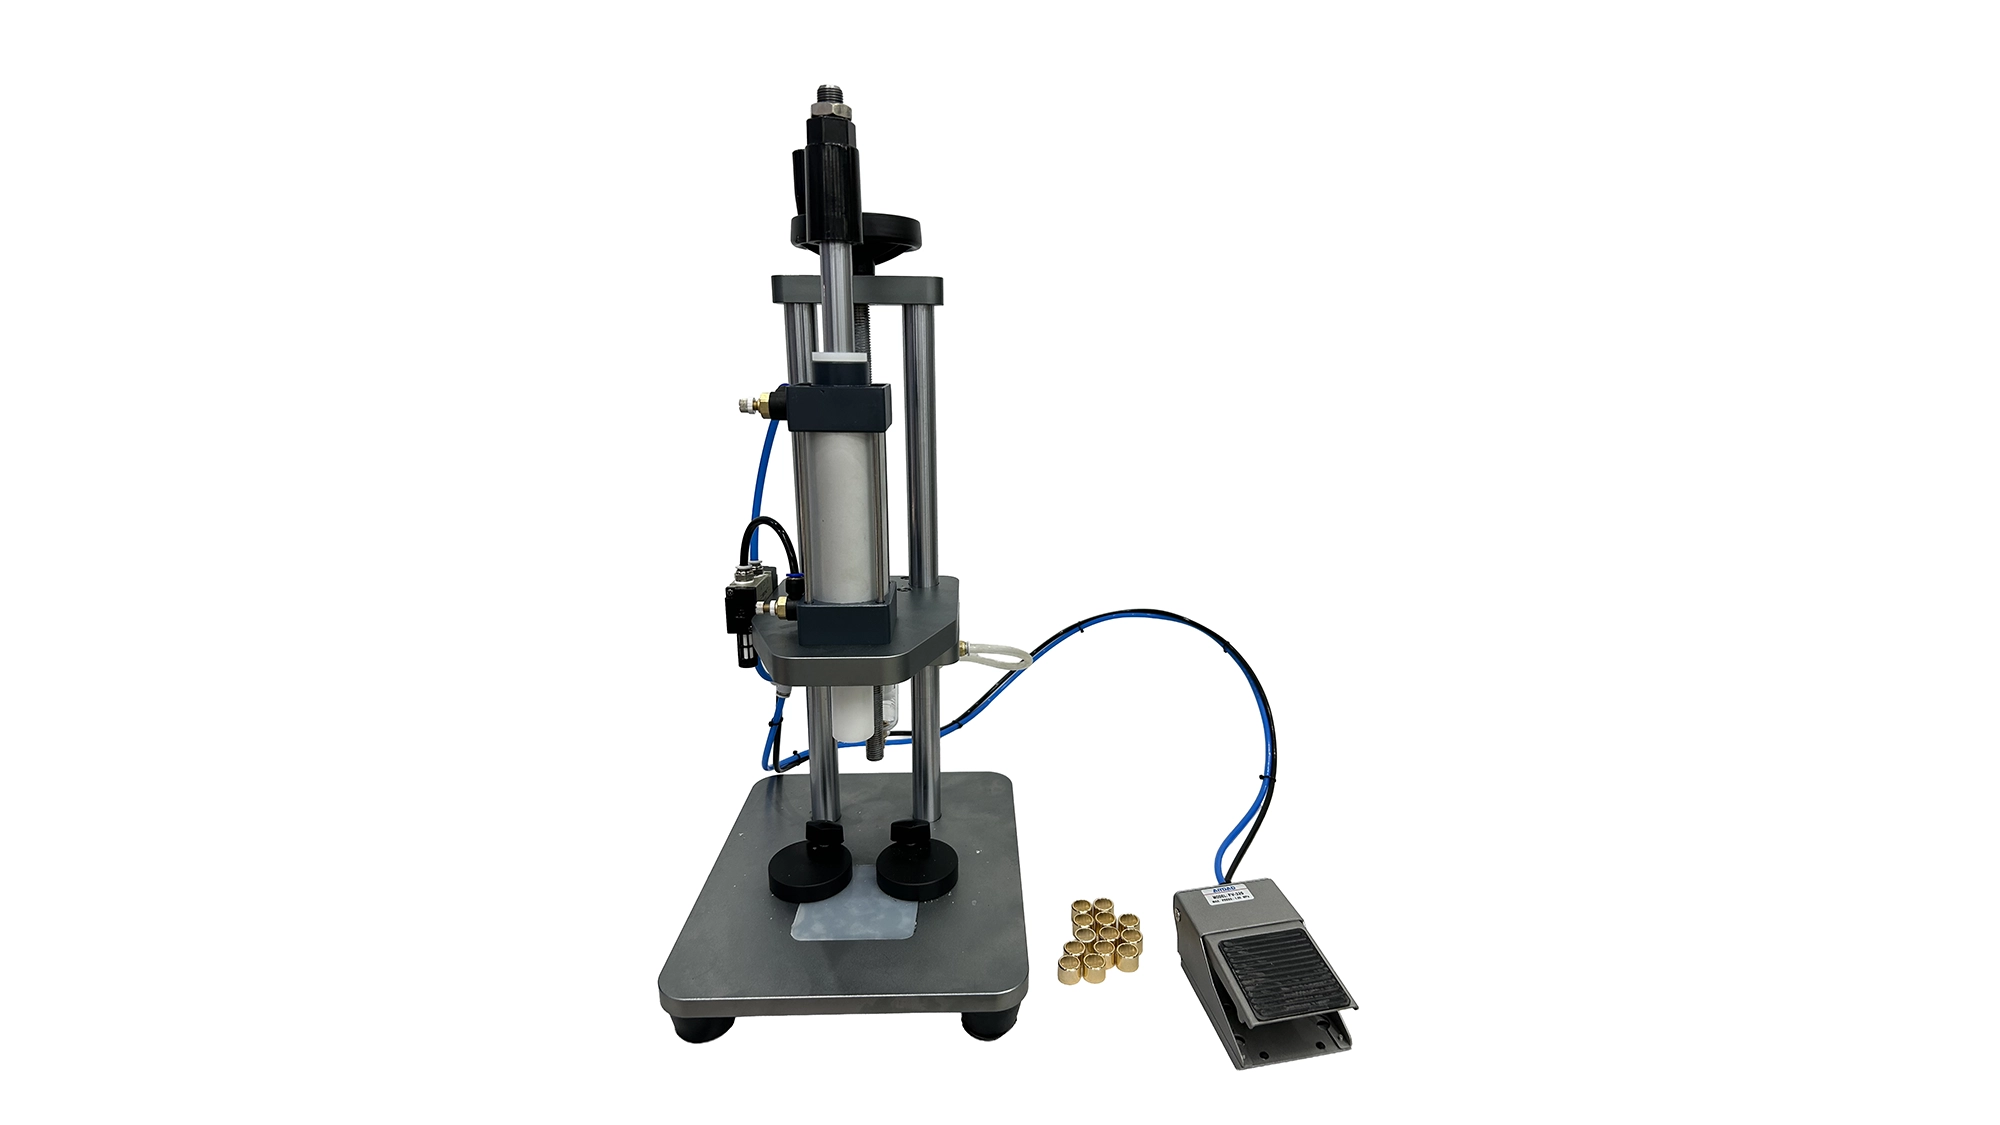
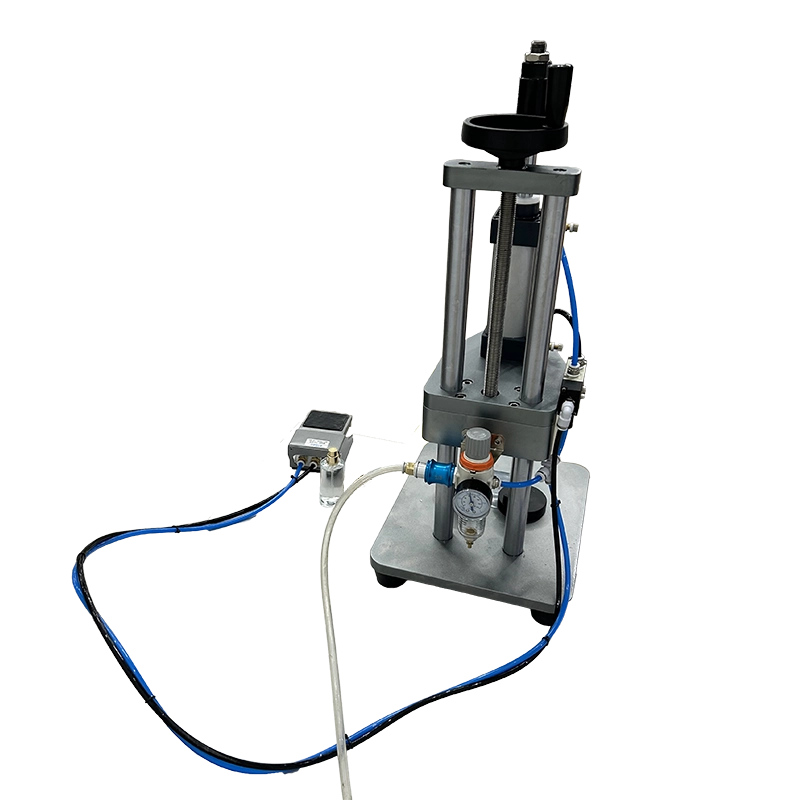
The Perfume Bottle Collar Pressing Machine presses compatible aluminum decorative collars onto glass bottles after the pump has been secured. Pneumatic operation, pedal control and manual height adjustment support operator-assisted assembly. A size-matched pressing head and adjustable bottle holder position the package for each cycle. Within the perfume production equipment range, this benchtop machine performs collar fitting as a separate packaging operation.
| Production Speed (BPM) | 15-30 | Air Pressure | 0.4–0.8 MPa |
| Machine Frame Material | SUS304 Stainless Steel Frame | Drive Type | Pneumatic |
| Capping Method | Constant-Force Pneumatic Capping | Installation Type | Benchtop |
| Capping Principle | Collar Pressing | Automation Level | Semi-Automatic |
| Capping Head/Heads | 1 | Control System | Pedal |
| Cap Size Range (Ø=mm) | 1-80 | Machine Dimensions(L*W*H)mm | 310mm*260mm*510mm |
| Capping Torque Range (Nm) | (Adjustable) | Machine Weight (kg) | 13 |
| Pneumatic Brand | AirTAC | ||
Product Gallery
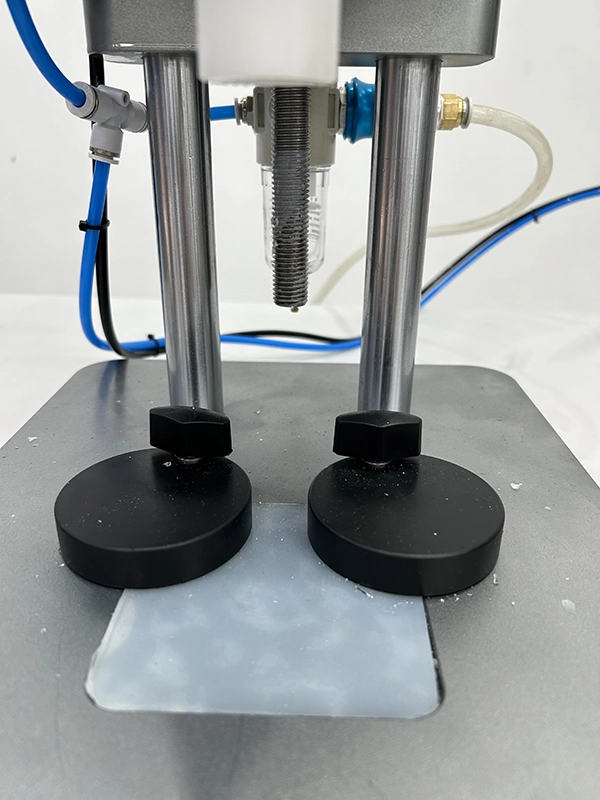
Product Overview
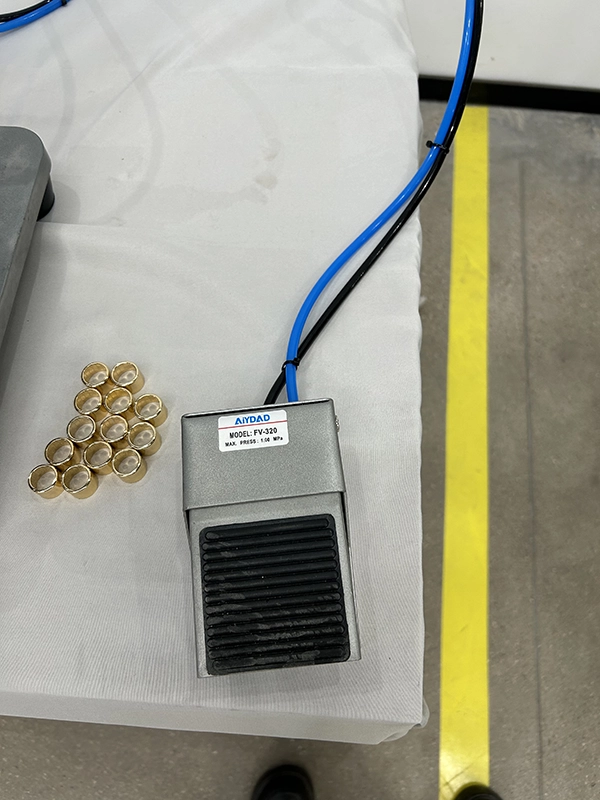
This semi-automatic machine fits aluminum decorative collars to compatible glass perfume bottles. The operator places the collar over the secured pump assembly, positions the bottle in its holder and activates the pneumatic press through the pedal.
For perfume and fragrance packaging, the collar forms part of the finished bottle’s appearance. Its fit, seating position and surface condition should be assessed with the bottle and pump as a complete package.
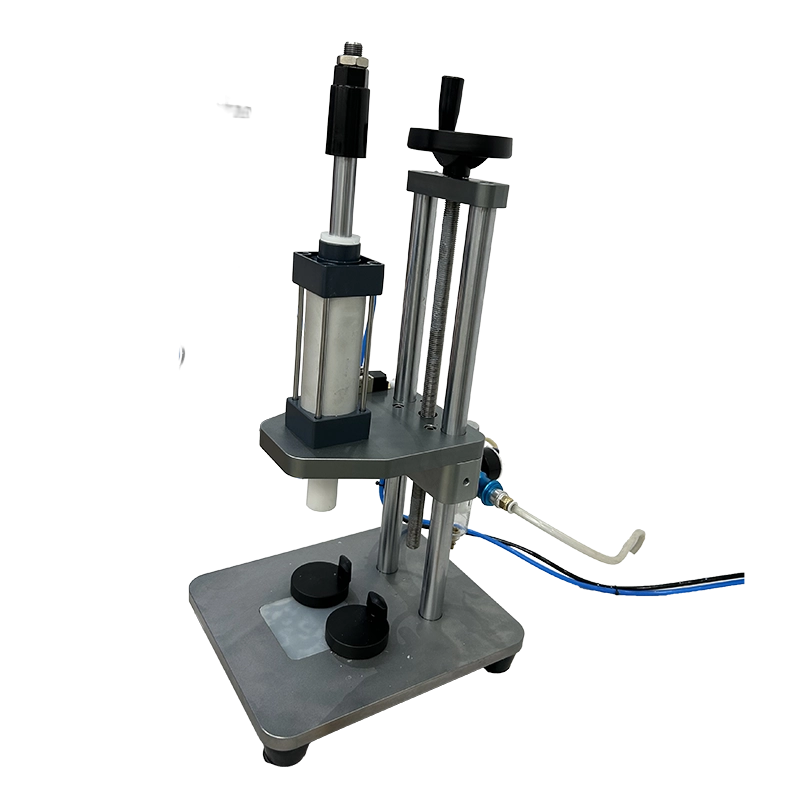
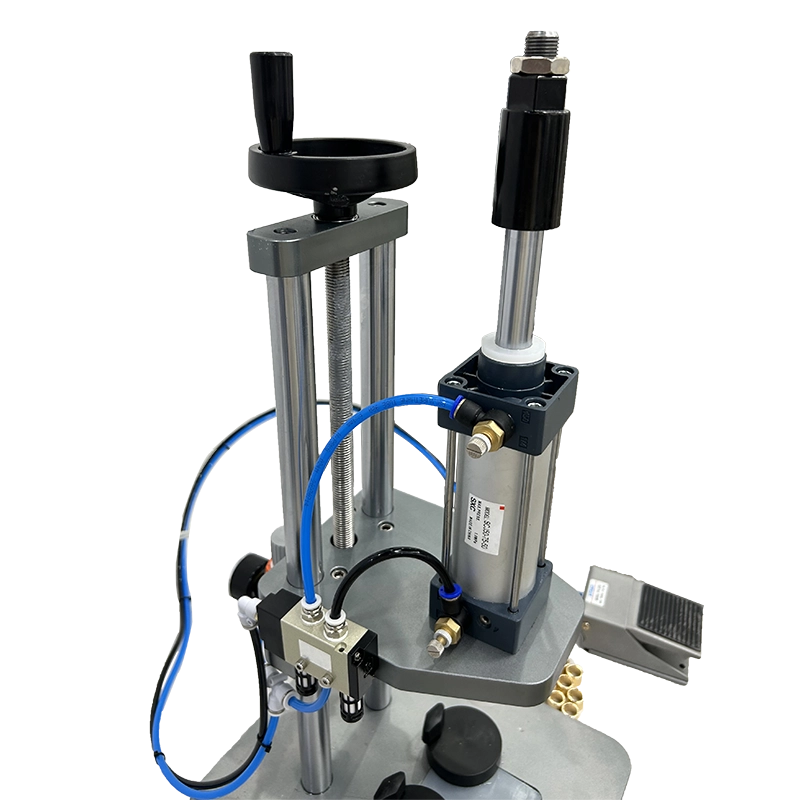
The single-head benchtop arrangement uses manual height adjustment and an adjustable bottle holder. Pressing force can be adjusted for the approved collar and package, while the pressing head or mold is matched to the collar size.
The rated production speed is 15–30 bottles per minute. Actual output depends on collar placement, bottle positioning and the operator’s handling sequence.
This machine performs decorative collar pressing after pump attachment. It does not replace perfume-pump crimping or provide the bottle’s primary liquid seal. Collar fitting and closure integrity remain separate packaging requirements.
Machine Configuration
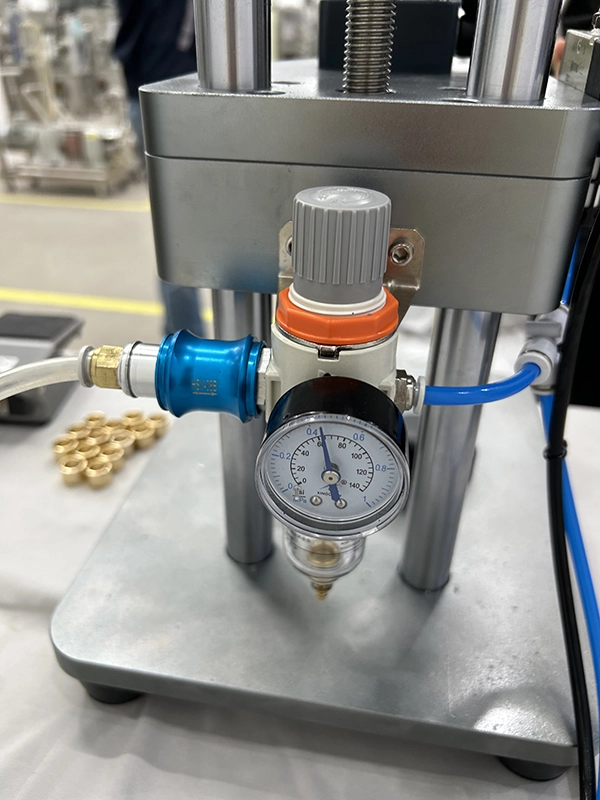
A SUS304 stainless steel frame supports a single pneumatic pressing assembly above the bottle-positioning area. AirTAC pneumatic components provide the supplied actuation, with a pedal used to initiate the pressing cycle.
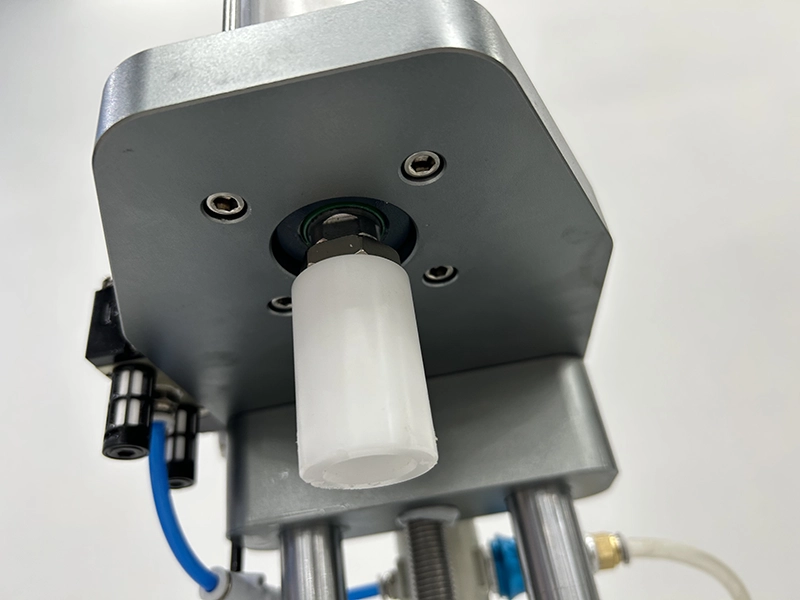
The pressing head or mold is selected to match the decorative collar. Manual height adjustment positions the working assembly around the bottle and pump, while the adjustable holder supports and locates the package beneath the head.
Pressing force is adjustable. The operating setup combines the selected head, bottle position and force setting to achieve the required collar seating.
The machine is designed for benchtop installation. Operators place collars and load and remove bottles manually. Different collar sizes or profiles may require another pressing head and a revised bottle-holder setup.
The complete bottle, secured pump and collar are used together when preparing a packaging format.
Key Features
- Pneumatic pressing fits decorative collars after the pump has been secured.
- A single pressing head provides a dedicated collar-assembly station.
- Pedal control initiates the supplied pressing cycle.
- Manual height adjustment accommodates the approved bottle and pump arrangement.
- An adjustable holder positions the bottle beneath the pressing head.
- Size-matched heads or molds support different approved collar formats.
- Adjustable pressing force supports package-specific setup.
- The benchtop frame provides a compact station for operator-assisted packaging.
Applications
- Perfume & Fragrance Products
Recommended Machines

300L Perfume Making Machine with Chilling Freezing Filtration & Pneumatic Agitator for Eau de Toilette, Cologne & Essential Oil Processing
View Details
Semi-Automatic Perfume Bottle Crimping Machine for Perfume, Fragrance, Cosmetic Spray Bottles and Aluminum Pump Caps
View Details
Working Principle
The bottle reaches the collar-pressing station with its pump already secured. The operator places the compatible aluminum collar over the pump assembly and positions the bottle in the adjustable holder.
The pressing head or mold is prepared for the collar size and profile. Manual height adjustment aligns the working assembly with the package, and the pressing force is set for the intended fit.
Pedal activation initiates the pneumatic pressing cycle. The head applies the pressing action to seat the collar around the pump assembly. Bottle support and alignment help maintain the intended relationship between the collar, pump and glass container.
After the cycle has completed and the head is clear, the operator removes the bottle and checks the collar’s seating and appearance.
The next bottle is loaded through the same sequence. Production pace depends on collar presentation, package positioning, cycle operation and finished-bottle handling.
When changing collar format, the appropriate head or mold is installed and the bottle position and pressing setup are reviewed. Representative packages are checked before routine production resumes.
Where the package uses a crimped spray pump, a separate perfume bottle crimping machine performs that attachment before decorative collar fitting.
Suitable Products
| Warranty | 24 Months | Payment Terms | 40% T/T Deposit, 60% Balance Before Shipment (Alibaba Trade Assurance Available) |
| Lead Time | 15–20 Working Days | Packaging | Standard Export Fumigation-Free Wooden Case |
After-Sales & Technical Support
🔧 Common Problems
Possible operating symptoms include collars sitting at different heights, uneven seating, visible gaps or a tilted finished appearance. Operators may observe marks on the collar, contact marks on the bottle, distortion of the decorative component or interference with the pump assembly. Bottles may sit inconsistently in the holder or move during pressing. Other observations include irregular head travel, slow return, inconsistent pedal response or audible pneumatic leakage. A change of collar format may also produce a different fit or contact pattern from the previous setup. Record the bottle, pump, collar, pressing head and operating setup when investigating an observation.
🛠 Troubleshooting
Problem: The collar does not seat fully. Possible Cause: Component fit, head profile, working position or pressing force is unsuitable. Recommended Solution: Check the complete package and approved tooling before increasing force.Problem: The collar sits unevenly. Possible Cause: Bottle positioning, collar presentation or head alignment differs from the approved setup. Recommended Solution: Stop the machine and review the holder and head position.Problem: The collar shows marks or deformation. Possible Cause: Deposits, damaged tooling or excessive contact force affects pressing. Recommended Solution: Isolate the equipment before inspecting and cleaning the contact surfaces.Problem: The bottle moves during pressing. Possible Cause: The holder does not provide suitable positioning for the package. Recommended Solution: Review the support arrangement using representative bottles before restarting.Problem: The pressing head contacts the pump. Possible Cause: The tool or clearance does not suit the complete assembly. Recommended Solution: Stop production and review the matched head and package geometry.Problem: Head movement or pedal response becomes irregular. Possible Cause: Air-supply conditions, an obstruction or a pneumatic component fault interrupts operation. Recommended Solution: Stop the machine and arrange inspection through the approved service procedure.
🧼 Cleaning Method
1. Stop production through the approved shutdown procedure. 2. Remove bottles and collars from the working area. 3. Isolate the compressed-air supply before manual access. 4. Release retained pressure through the designated method. 5. Remove the pressing head where the cleaning procedure requires disassembly. 6. Clean the head’s contact surfaces using an approved compatible method. 7. Clean the bottle holder and support area. 8. Remove deposits from accessible frame surfaces. 9. Wipe the pedal exterior through the permitted method. 10. Inspect cleaned surfaces for residue or damage. 11. Dry serviced components according to the approved procedure. 12. Refit the pressing head using the specified attachment method. 13. Complete the required function and package checks before production.
📋 Maintenance
1. Establish the service schedule from the supplied component documentation. 2. Isolate the compressed-air supply before service access. 3. Release retained pressure through the approved procedure. 4. Inspect the pressing head for wear, damage or deposits. 5. Check the head attachment according to the service instructions. 6. Examine the bottle holder for looseness or worn contact surfaces. 7. Inspect manual height-adjustment attachments for deterioration. 8. Check pneumatic tubing and fittings for visible damage. 9. Service AirTAC components according to their identified instructions. 10. Inspect the pedal and its connections through the approved method. 11. Maintain installed air-treatment components where fitted. 12. Check the machine’s bench attachment or restraint. 13. Verify the approved setup with representative packages. 14. Record findings against the affected tool or component.
⚙️ Installation
1. Review the machine instructions and approved package samples. 2. Prepare a stable workbench with suitable operating access. 3. Inspect the delivered machine for visible transport damage. 4. Position the machine using the designated handling method. 5. Secure the assembly according to the installation instructions. 6. Position the pedal for deliberate operation. 7. Connect regulated compressed air according to the pneumatic schedule. 8. Install the pressing head matched to the collar. 9. Prepare the adjustable holder for the glass bottle. 10. Set the working height around the assembled bottle and pump. 11. Check clearance through the pressing movement. 12. Establish the pressing-force setting using representative components. 13. Verify operation through the approved commissioning procedure. 14. Inspect collar seating and the completed package condition. 15. Record the approved format setup before routine production.
🔩 Spare Parts
Why Choose This Machine
- A focused finishing operation: The machine gives decorative collar fitting its own setup and inspection point after the pump has been attached.
- Package-specific tooling: A head or mold matched to the collar helps define where the pressing action contacts the component.
- Adjustable setup: Manual height positioning, the bottle holder and adjustable force allow the station to be prepared around the approved package.
- Compact installation: The benchtop arrangement fits into an operator-assisted packaging area without requiring a dedicated conveyor connection.
- Flexible production scheduling: Bottles can be presented individually, supporting work organized around different fragrance batches and packaging formats.
- Separate appearance checks: Collar seating, alignment and surface condition can be reviewed independently from pump attachment and filling quantity.
Frequently Asked Questions
Installation Requirements
Position and secure the machine according to its installation instructions. Place the pedal where it can be operated deliberately without obstructing normal movement.
Provide a regulated compressed-air supply within the specified 0.4–0.8 MPa range. Air consumption and treatment requirements follow the final pneumatic schedule.
Arrange the work area so operators can present bottles through the designated loading position. Keep access to moving components controlled according to the machine’s operating provisions.
Prepare the correct pressing head or mold for each approved collar. Provide representative glass bottles with their pumps secured, together with the production collars.
Allow safe access for manual height adjustment and bottle-holder setup. Changes to tooling or position should follow the approved isolation procedure.
Provide suitable lighting for checking collar seating, alignment and visible surface condition. Place upstream pump-attachment and downstream collection tasks so bottles can be handled without unnecessary transfers.
Related Articles


Technical Buyer's Handbook & Deep Insight
Ready to Get a Quote?
Contact our team directly for pricing, customization options, and delivery timelines.
💬 WhatsApp Us NowGet Your Download Link
Please fill in your details and we'll send the download link to your email.