
Automatic Servo 4-Wheel Capping Machine for Screw Caps, Trigger Sprayers & Pumps in Cosmetic, Food & Chemical Industry
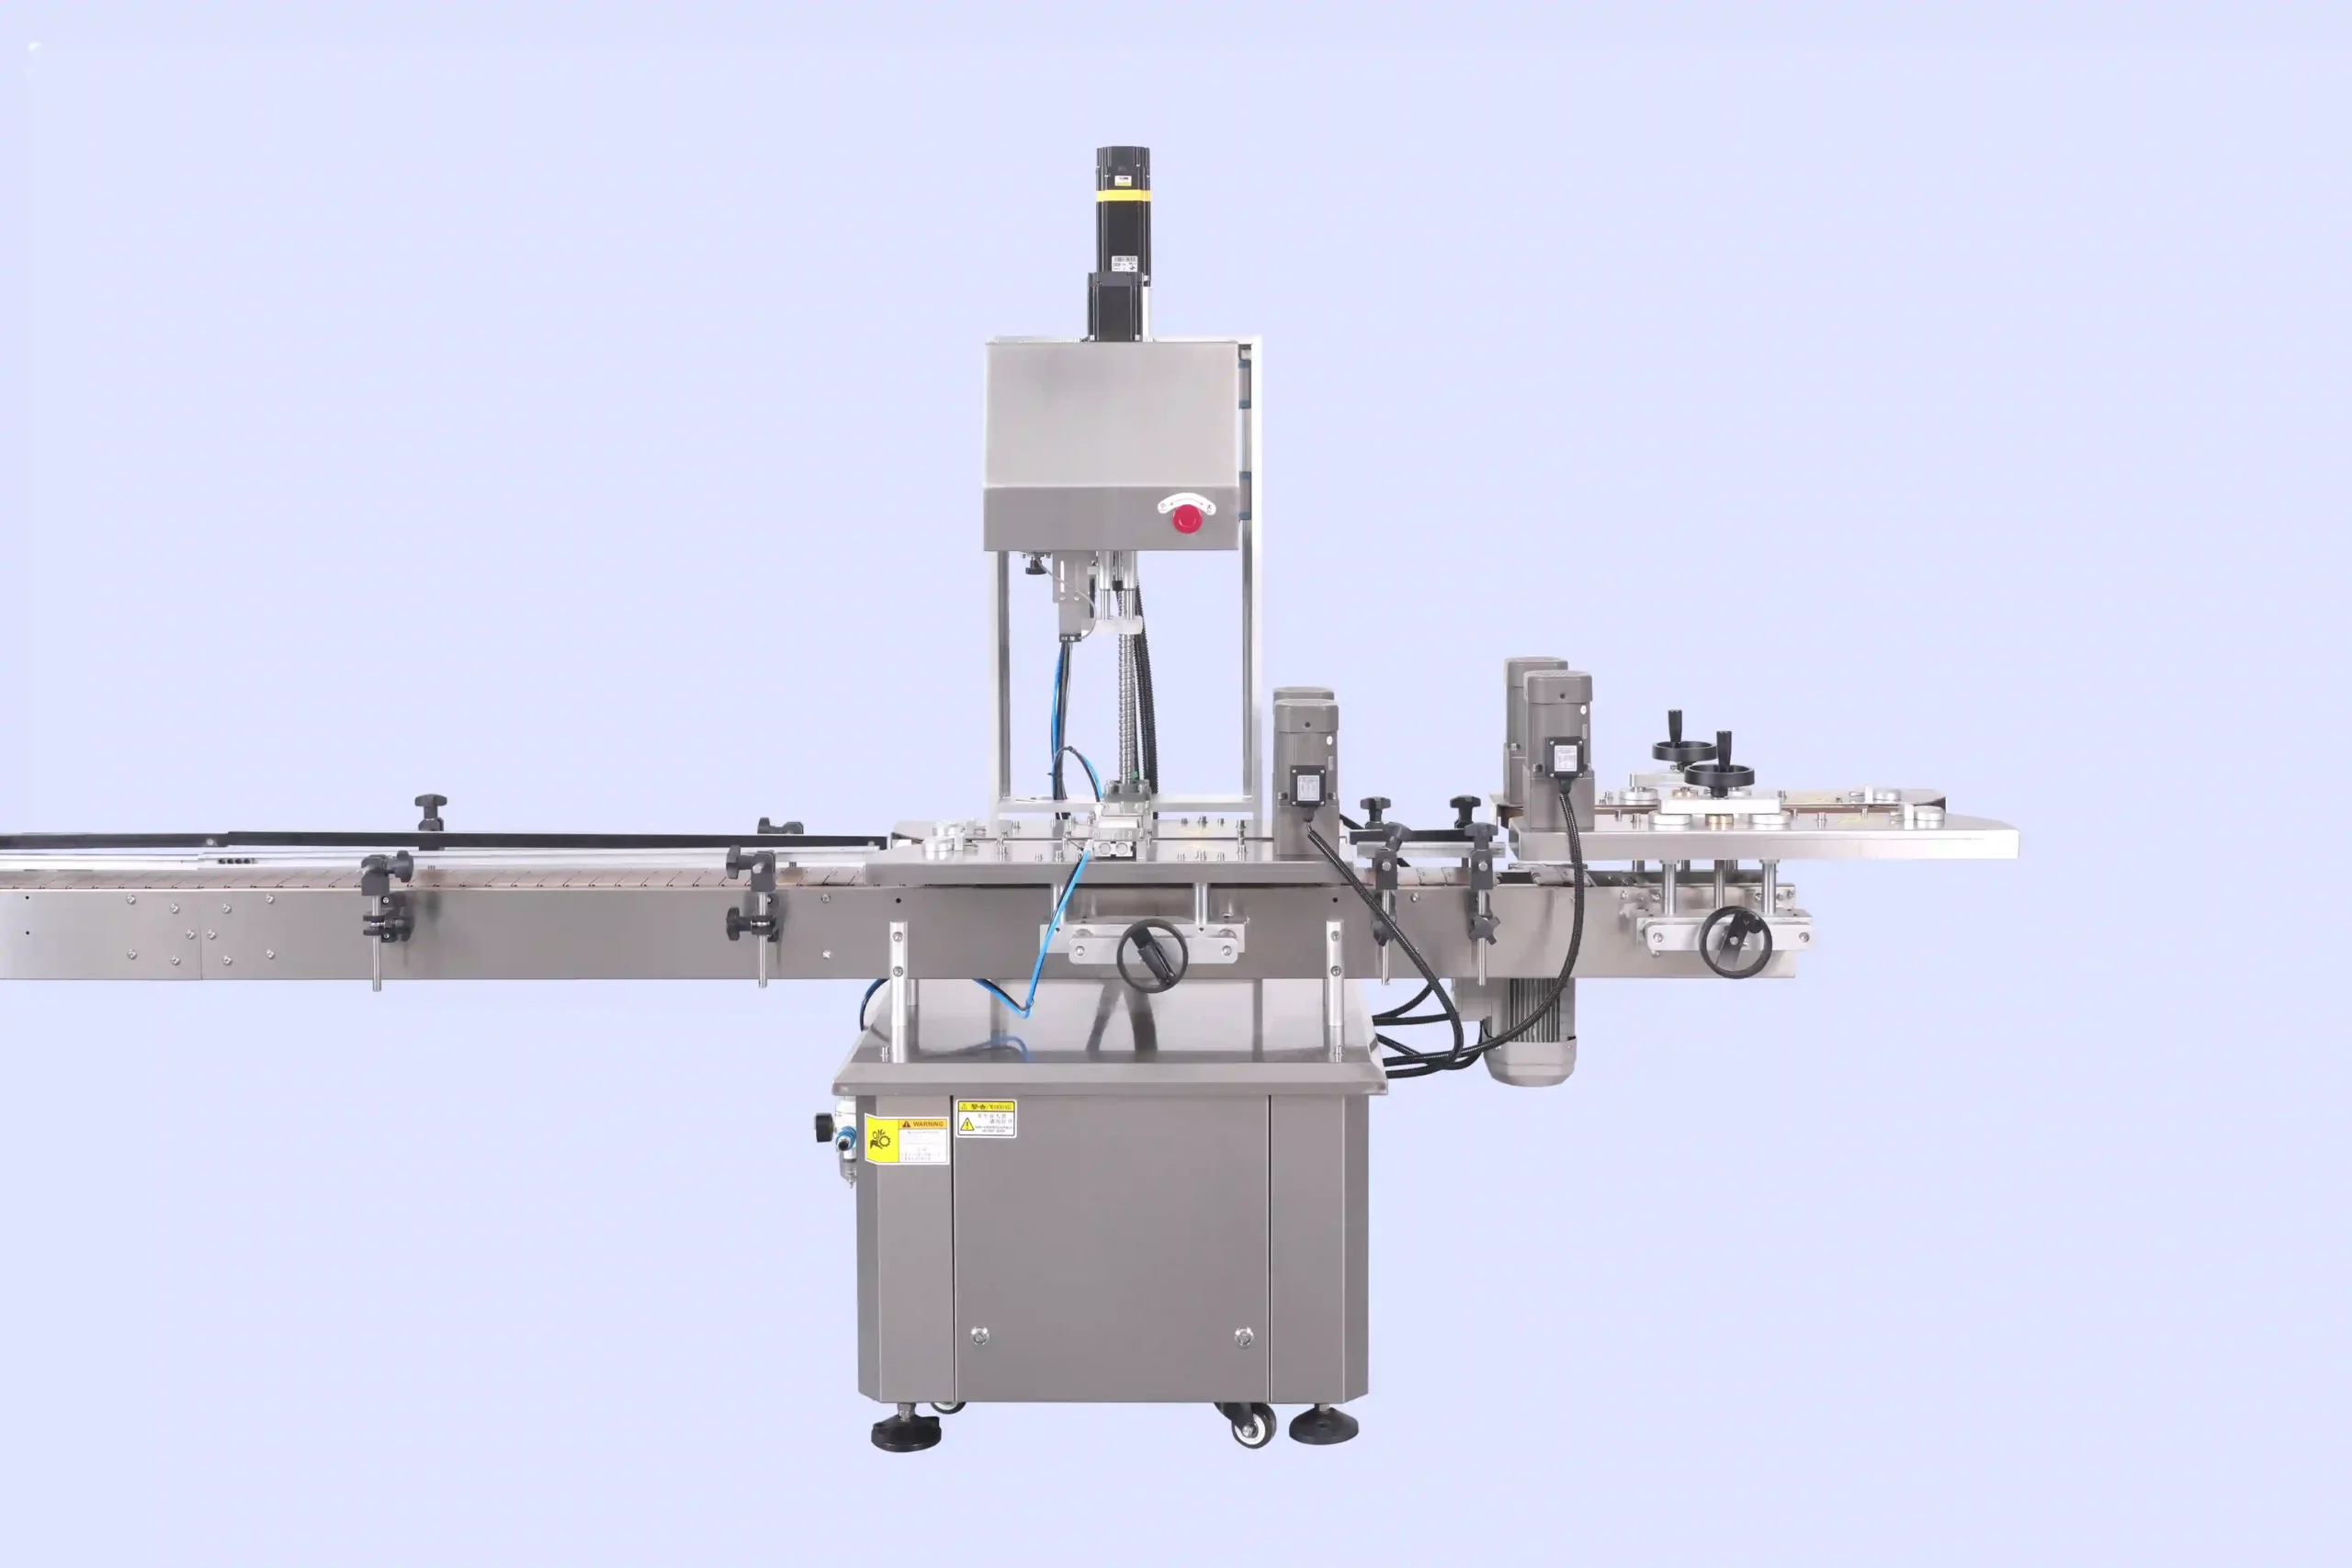
The Servo 4-Wheel Capping Machine tightens compatible screw caps, trigger sprayers and pump closures using four silicone contact wheels and belt-supported bottle handling. Servo torque control and servo-driven height adjustment support setup for different packages. Automatic cap feeding and placement are supplied, with manual cap placement also available. This linear configuration forms part of the capping machines range for cosmetic, food and chemical packaging.
| Production Speed (BPM) | 40-80 | Pneumatic Brand | AirTAC |
| Contact Material | Silicone (Food Grade) | Cylinder Brand | Airtac |
| Machine Frame Material | SUS304 Stainless Steel Frame / Aluminum Alloy | Photoelectric Brand | Panasonic |
| Servo Motor Brand | Other / Customer Specified | Voltage | Configurable to local grid (110V–480V, 50/60Hz, Single or 3-Phase) |
| Conveyor System | POM Slat Chain Conveyor / SUS304 Stainless Steel Chain (Optional) | Total Power (kW) | 2 |
| Capping Method | Servo-Driven Torque Capping | Air Pressure | 0.4–0.8 MPa |
| Machine Layout Type | Linear Capping Machine | Drive Type | Electro-Pneumatic Combined |
| Capping Principle | 4-Wheel Capping | Installation Type | Mobile (Caster-Mounted) |
| Capping Head/Heads | 1 | Automation Level | Fully Automatic |
| Cap Size Range (Ø=mm) | 20-60 | Electrical Components | Top-tier Chinese Brand: DELIXI / CHINT / People Electric / TENGEN |
| Torque Control | Servo Precision Torque Control | Control System | PLC + HMI Touch Screen Control |
| Capping Torque Range (Nm) | (Adjustable) | PLC System | INOVANCE/Xinje or equivalent brand |
| Capping Head Lift Type | Servo-driven Lift | HMI / Touch Screen | Kinco/MCGS/INOVANCE/Xinje/Flexem or equivalent brand |
| Anti-Scratch Protection | Anti-Scratch Nylon / PTFE Chuck Lining Included | Machine Dimensions(L*W*H)mm | 2000*760*1500 |
| Bottle Gripping Module | Belt Gripping Conveyor | Machine Weight (kg) | 220 |
Product Video
Product Overview
The Servo 4-Wheel Capping Machine tightens compatible screw caps, trigger sprayers and pump closures using four silicone contact wheels and belt-supported bottle handling. Servo torque control and servo-driven height adjustment support setup for different packages. Automatic cap feeding and placement are supplied, with manual cap placement also available. This linear configuration forms part of the capping machines range for cosmetic, food and chemical packaging.
Machine Configuration
A linear conveyor presents bottles to a single four-wheel capping station. Four silicone contact wheels apply the tightening action, while the belt-gripping module supports the bottle against rotation.
The capping assembly combines servo torque control with servo-driven lift adjustment. Automatic cap feeding and placement serve the approved closure format; manual placement can also be used.
PLC and HMI controls coordinate the supplied functions. Panasonic photoelectric components and AirTAC pneumatic components support sensing and actuation. The servo motor, PLC, HMI and electrical components are selected for the ordered configuration.
The frame combines SUS304 stainless steel and aluminum-alloy construction on a caster-mounted base. A POM slat-chain conveyor provides bottle transport, with a stainless steel chain option available. Bottle guides, gripping-belt settings and wheel position are prepared around the actual bottle and closure.
Key Features
- Four silicone wheels tighten closures through their circular contact surface.
- Servo torque adjustment supports package-specific tightening settings.
- Servo-driven lift positions the capping assembly for bottle-height changes.
- Gripping belts support bottles against rotation during cap tightening.
- Automatic cap feeding and placement reduce routine closure-loading tasks.
- Manual cap placement remains available for suitable operating arrangements.
- Compatible trigger sprayers and pumps can be tightened around their circular closure section.
- PLC and HMI controls bring setup and operating functions into one interface.
Applications
- Cosmetic Cream & Lotion, and Skin Care
- Detergents, Liquid Washing & Household Cleaning
- Hair Care, Personal Care & Body Wash
Recommended Machines

Working Principle
Bottles enter the linear conveyor with the selected closure supplied through the automatic feeding and placement arrangement, or presented manually. The package is guided toward the four-wheel tightening station.
The bottle-gripping belts support the container and resist the rotation created during tightening. Their position and grip are set around the bottle’s shape and rigidity.
Four silicone wheels contact the circular closure surface and turn the cap onto the bottle thread. The servo-controlled tightening setting is established for the approved bottle and closure combination.
For trigger sprayers and pump closures, the wheels act on the suitable circular tightening section. Projecting components need clearance through the handling route, while cap presentation must allow the thread to engage correctly.
Servo-driven lift positions the assembly for the selected bottle height. Wheel spacing, guides and gripping settings are prepared before production, followed by checks of cap engagement and the finished package.
After tightening, bottles continue along the conveyor to collection or downstream packaging. PLC and HMI controls coordinate the supplied sequence. Each new format is checked with representative bottles and closures before routine operation.
Suitable Products
| Warranty | 24 Months | Payment Terms | 40% T/T Deposit, 60% Balance Before Shipment (Alibaba Trade Assurance Available) |
| Lead Time | 15–20 Working Days | Packaging | Standard Export Fumigation-Free Wooden Case |
After-Sales & Technical Support
🔧 Common Problems
Possible operating symptoms include caps finishing at different positions, tilted closures, incomplete thread engagement or inconsistent results during package torque checks. Bottles may rotate between the gripping belts, become unstable during transfer or show visible contact marks. Operators may observe silicone-wheel slipping, cap scuffing, deformation of lightweight bottles or difficulty passing a trigger or pump assembly through the working area. Feeding-related observations can include interrupted cap supply, irregular placement or repeated stops at a particular closure format. Other symptoms include uneven conveyor movement, irregular height adjustment, audible pneumatic leakage or repeated HMI messages. Record the bottle and closure combination, operating settings, speed and affected stage when investigating an observation.
🛠 Troubleshooting
Problem: Caps do not tighten consistently. Possible Cause: Wheel contact, bottle grip, cap condition or the operating setup varies. Recommended Solution: Compare the package and settings with the approved format record before changing torque settings.Problem: Bottles rotate during tightening. Possible Cause: Belt position, grip or bottle geometry provides insufficient support. Recommended Solution: Stop the equipment and review the gripping setup without distorting the container.Problem: Caps finish tilted or cross-threaded. Possible Cause: Closure presentation, bottle positioning or component compatibility is unsuitable. Recommended Solution: Check cap placement and representative packaging components before adjusting the tightening station.Problem: Caps or bottles show visible marks. Possible Cause: Contamination, worn contact surfaces or excessive contact force affects handling. Recommended Solution: Isolate the machine before inspecting and cleaning the wheels and belts.Problem: Cap supply becomes irregular. Possible Cause: A feed obstruction, mixed components or an unsuitable format setup interrupts presentation. Recommended Solution: Stop the feeder and inspect it through the approved access procedure.Problem: A trigger or pump contacts the machine structure. Possible Cause: The complete closure assembly lacks clearance in the current setup. Recommended Solution: Stop production and review the format arrangement before restarting.Problem: The machine repeatedly pauses. Possible Cause: A required detection condition or operating permission is absent. Recommended Solution: Read the HMI message and correct the identified condition without bypassing protections.
🧼 Cleaning Method
1. Stop production through the approved shutdown sequence. 2. Remove bottles and closures from the designated working positions. 3. Isolate electrical and pneumatic energy before manual access. 4. Release retained pressure through the approved procedure. 5. Remove loose closures from the feeding and placement areas. 6. Remove designated detachable contact parts according to their instructions. 7. Clean the silicone capping-wheel surfaces using an approved compatible method. 8. Clean bottle-gripping belts without damaging their contact surfaces. 9. Clean bottle guides and accessible conveyor surfaces. 10. Clean cap-feeding and placement components through their permitted access method. 11. Remove residue from accessible frame and collection areas. 12. Wipe sensing surfaces according to the component instructions. 13. Inspect contact surfaces for remaining residue or cleaning-agent deposits. 14. Dry cleaned components according to the approved method. 15. Reassemble removed parts using the specified fitting procedure. 16. Perform the required post-cleaning function checks before production resumes.
📋 Maintenance
1. Establish the service schedule from the installed component documentation. 2. Isolate electrical and pneumatic energy before accessing service assemblies. 3. Release retained pressure through the approved procedure. 4. Inspect silicone capping wheels for wear, hardening or surface damage. 5. Examine bottle-gripping belts for wear, contamination or deterioration. 6. Check wheel attachments according to the supplied service instructions. 7. Inspect bottle guides and accessible conveyor attachments for looseness. 8. Examine cap-feeding and placement parts for wear or obstruction. 9. Service the height-adjustment assembly according to its component documentation. 10. Inspect accessible drive connections through the approved access method. 11. Clean Panasonic photoelectric sensing surfaces using the permitted procedure. 12. Check AirTAC pneumatic tubing and fittings for visible damage. 13. Service installed cylinders according to their identified instructions. 14. Arrange qualified inspection of electrical terminals and protective devices. 15. Verify the tightening setup through the approved package-check method. 16. Test supplied stop functions using the designated functional procedure. 17. Inspect caster restraints before returning the machine to operation. 18. Record findings against the affected format, station or component.
⚙️ Installation
1. Review the approved layout and packaging-format drawings. 2. Verify the delivery route against the final transport envelope. 3. Obtain approval of the supporting surface for the operating load. 4. Inspect delivered assemblies for visible transport damage. 5. Position the machine using the designated handling method. 6. Secure the caster-mounted base at its operating location. 7. Connect upstream and downstream conveyors according to the layout. 8. Arrange electrical connection by qualified personnel using the final wiring schedule. 9. Verify protective earthing before electrical commissioning. 10. Connect the regulated compressed-air supply according to the pneumatic schedule. 11. Prepare the bottle guides for the approved container. 12. Set the gripping belts around the bottle’s suitable support area. 13. Position the capping assembly using the supplied height adjustment. 14. Prepare the wheel spacing for the selected closure. 15. Set up automatic cap feeding and placement for the approved format. 16. Verify clearance for trigger or pump projections where applicable. 17. Test supplied detection and stop functions. 18. Establish the tightening setting using representative packages. 19. Check closure application through the agreed acceptance method. 20. Document the approved format setup before routine production.
🔩 Spare Parts
Why Choose This Machine
- One tightening approach for several closure styles: Four-wheel contact accommodates suitable screw caps and the circular tightening sections of compatible trigger sprayers and pumps.
- Package-specific adjustment: Servo torque settings allow the tightening setup to be developed around the actual closure, bottle and required finished condition.
- Supported bottle handling: Gripping belts resist bottle rotation during tightening, making bottle support part of the capping setup rather than an afterthought.
- Flexible cap presentation: Automatic feeding and placement serve routine production, while manual placement provides another operating option for suitable formats.
- Practical height conversion: Servo-driven lift assists positioning when changing bottle height, alongside the required guide, belt and wheel adjustments.
- Linear line connection: Conveyor transport provides a straightforward equipment interface between filling and downstream package handling when bottle presentation and spacing are matched.
Frequently Asked Questions
Installation Requirements
Provide a level supporting surface and secure the caster-mounted base at its operating location. Position connected conveyors so bottles transfer smoothly into and out of the gripping and tightening section.
Prepare the electrical supply for the ordered voltage, frequency and phase configuration. The listed machine power is 2 kW. Use the final electrical schedule when preparing the connection and include any separately supplied auxiliary equipment.
Provide regulated compressed air within the specified 0.4–0.8 MPa range. Confirm airflow and air-treatment requirements from the pneumatic schedule before sizing the service.
Allow access to the automatic cap-feeding and placement assembly. The replenishment position should support routine work without requiring access to moving components.
Arrange representative bottles and closures for setup and commissioning. Prepare a designated area for checking the finished cap condition and carrying out the agreed torque checks.
For products requiring special installation conditions, assess the capping station together with the surrounding filling and packaging equipment.
Related Articles


Technical Buyer's Handbook & Deep Insight
Ready to Get a Quote?
Contact our team directly for pricing, customization options, and delivery timelines.
💬 WhatsApp Us NowGet Your Download Link
Please fill in your details and we'll send the download link to your email.