
Automatic Servo Cartridge Filling & Stoppering Machine for Dental Cartridges, Injectable Drugs, Hyaluronic Acid, Beauty Serum and Biopharmaceutical Products
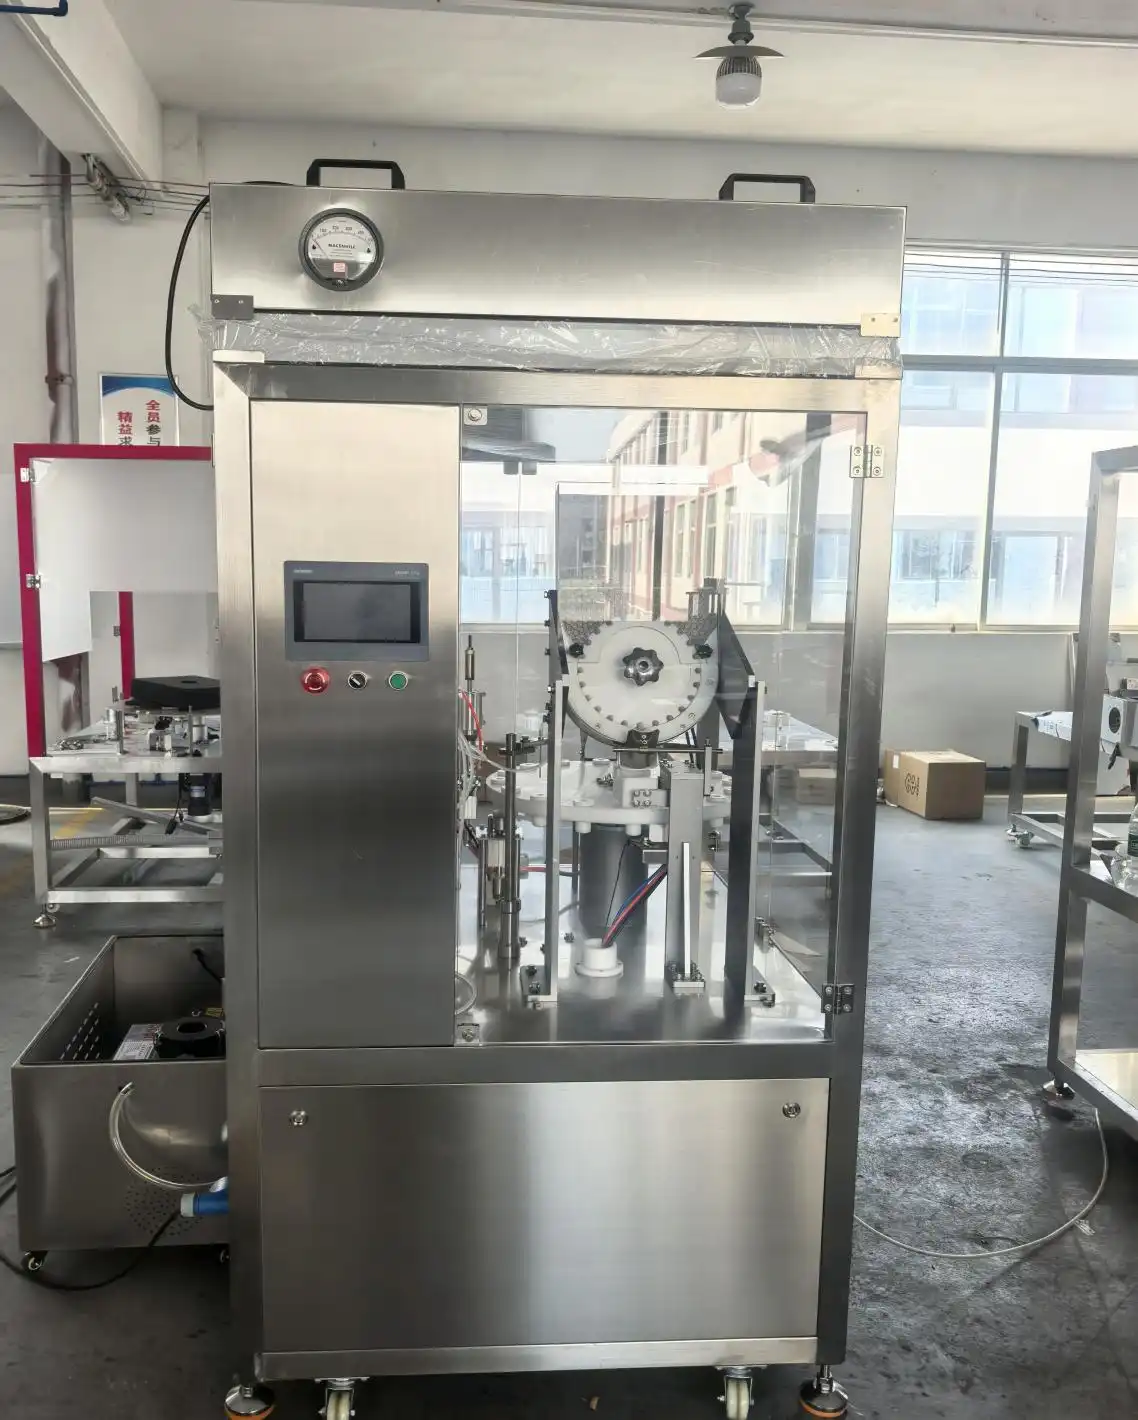
The Servo Cartridge Filling and Stoppering Machine automatically fills compatible liquids into preclosed glass cartridges and inserts rubber piston stoppers under vacuum. Operators replenish the cartridge hopper and stopper bowl, while the machine handles feeding, rotary indexing, peristaltic dosing, stoppering, and finished-product discharge. Applications include dental cartridge preparations, selected pharmaceutical liquids, compatible hyaluronic acid formulations, and beauty serums, subject to product and packaging assessment.
| Integrated Functions | Bottle Feeding / Rotary Indexing / Automatic Filling | Motor Brand | Top-Tier Chinese Servo (Inovance / Equivalent) |
| Filling Principle | Peristaltic Pump | Servo Drive Type | Servo-driven Filling Pump Motor / Servo-driven Conveyor Belt Motor |
| Output Configuration | 1-out | Photoelectric Brand | Panasonic |
| Machine Layout Type | Rotary Filling Machine | Pneumatic Components Brand | AirTAC |
| Container Type | Cartridge | Cylinder Brand | Airtac |
| Container Material | Glass / Aluminum / Rubber | fill_electrical_components | Schneider / Siemens / Omron (Optional/Customizable) |
| Filling Volume Range (ml) | 1ml~10ml | Voltage | Configurable to local grid (110V–480V, 50/60Hz, Single or 3-Phase) |
| Filling Accuracy | ±0.5% | Total Power (kW) | 3.5 |
| Filling Head/Heads | 1 | Air Pressure | 0.4–0.8 MPa |
| Filling Nozzle Movement | Fixed Type | Drive Type | Electro-Pneumatic Combined |
| Nozzle Type | Pneumatic Shut-off Nozzles (Anti-Drip) | Installation Type | Mobile (Caster-Mounted) |
| Drip Prevention | Pneumatic Anti-Drip Mechanism Included | Automation Level | Fully Automatic |
| Production Speed (Bottles Per Minute) | 10-15 | Control System | PLC + HMI Touch Screen Control |
| Feeding Method | Self-priming | PLC System | Siemens |
| With Machine Cover | Yes | HMI / Touch Screen | Siemens |
| Material Contact Parts | SUS316L Stainless Steel (Pharmaceutical Grade) | Machine Dimensions(L*W*H)mm | 1100x1050x2150 |
| Machine Frame Material | SUS304 Stainless Steel Frame | Machine Weight (kg) | 200 |
| Conveyor System | Conveyor Optional (POM Slat Chain, SUS304 Chain, PVC/PU Flat Belt) | ||
Product Overview
StriversMachinery’s automatic cartridge filler processes glass cartridges with one end already closed by an aluminum cap and diaphragm assembly. Liquid enters through the remaining open end, followed by insertion of the rubber piston stopper. The equipment brings these operations together without a separate aluminum-cap crimping station.
The cartridge format requires coordinated container presentation, small-volume dosing, and controlled stopper insertion. Hopper feeding and servo rotary indexing move cartridges between the processing stations, reducing individual handling during the production sequence. A finished-product conveyor receives discharged cartridges.
The equipment serves manufacturers evaluating cartridge packaging for dental preparations, pharmaceutical liquids, beauty serums, and compatible biopharmaceutical formulations. Hyaluronic acid products require assessment of their actual flow behavior rather than selection by ingredient name alone.
Peristaltic dosing and vacuum stoppering address different tasks: the pump delivers the liquid quantity, while the stoppering station reduces residual air between the liquid and inserted piston stopper. Product preparation, component preparation, environmental control, and production qualification remain part of the wider manufacturing arrangement.
Package samples and representative liquid are central to equipment assessment. Cartridge dimensions, the preclosed end, stopper geometry, and required finished condition must be reviewed together before the processing setup is finalized.
Machine Configuration
The machine combines a cartridge-loading hopper, automatic infeed, servo rotary indexing, a servo-driven peristaltic dosing module, and a vacuum stoppering station. A vibratory bowl presents rubber piston stoppers to the insertion mechanism, while automatic ejection transfers completed cartridges to the included finished-product conveyor.
Cartridge detection and a no-stopper alarm support supervision of the processing sequence. Fixed-position filling uses a pneumatic shut-off nozzle to control product release. Siemens PLC and touchscreen controls coordinate operation within the machine enclosure.
The frame is SUS304 stainless steel, with SUS316L stainless steel product-contact metal components. Flexible tubing and other nonmetallic contact components require separate compatibility selection. Panasonic photoelectric components and AirTAC pneumatic components form part of the configuration. Servo and electrical component selections follow the agreed order specification. The mobile structure supports positioning within a suitably prepared production area.
Key Features
- Hopper loading reduces the need to place each cartridge individually at the filling station.
- Servo rotary indexing presents cartridges to successive processing positions in a coordinated sequence.
- Peristaltic dosing transfers compatible liquids through a selected flexible product pathway.
- Vacuum stoppering reduces residual air between the liquid and inserted rubber piston stopper.
- Vibratory bowl feeding supplies piston stoppers to the automatic insertion mechanism.
- Cartridge detection supports monitoring of container presentation during the processing sequence.
- A no-stopper alarm draws operator attention to an interruption in stopper availability.
- Automatic ejection and the included conveyor move completed cartridges toward collection.
Applications
- Cosmetic Cream & Lotion, and Skin Care
- Pharmaceutical & Ointment Products
Recommended Machines

Automatic 2-Head Vial Liquid Filling Capping Machine with Rotary Bottle Unscrambler for Pharmaceutical, Cosmetics & Essential Oils
View Details
Automatic 2-Head Vial Powder Filling and Capping Machine with Rotary Infeed Table and Vacuum Powder Feeder for Pharmaceutical & Beauty Products
View Details

Working Principle
The cartridge filling and stoppering machine processes glass cartridges whose diaphragm end has already been closed. Filling and piston-stopper insertion take place through the opposite open end.
- Cartridge feeding: Operators replenish the hopper with compatible empty cartridges. The automatic infeed mechanism presents them to the rotary handling assembly.
- Servo indexing: The rotary system advances cartridges between processing positions. Cartridge detection supports monitoring of their presentation within the sequence.
- Liquid dosing: The servo-driven peristaltic pump progressively compresses flexible tubing to move liquid toward the fixed filling outlet. The pneumatic shut-off nozzle controls release at the end of the dosing cycle.
- Stopper presentation: The vibratory bowl feeds rubber piston stoppers to the insertion mechanism in the required orientation.
- Vacuum stoppering: The stoppering station establishes vacuum before pressing the piston stopper into the cartridge. This operation reduces residual air between the liquid and stopper; it is separate from liquid metering.
- Finished output: The ejection mechanism releases completed cartridges to the finished-product conveyor for collection or subsequent handling.
The PLC coordinates the sequence through the operating interface. A no-stopper alarm alerts the operator when stopper availability is interrupted. Vacuum operation is localized to stoppering; the equipment does not perform a separate bulk-product vacuum deaeration process. Aluminum-cap crimping is outside this machine’s processing sequence.
Optional Upgrades & Configurations
Custom Requirements
Corrosive-Resistant Construction for Strong Acids & Alkalis
Explosion-Proof Filling Systems for Flammable & Hazardous Environments
Custom Machine Layouts & Space-Saving Footprint Constraints
Extended & Custom-Length Long-Distance Conveyor Systems
Designated electrical component brands (Siemens PLC, Festo Pneumatics, etc.)
Irregular Bottle Shapes & Custom Packaging Solutions
Suitable Products
| Warranty | 24 Months | Payment Terms | 40% T/T Deposit, 60% Balance Before Shipment (Alibaba Trade Assurance Available) |
| Lead Time | 15–20 Working Days | Packaging | Standard Export Fumigation-Free Wooden Case |
After-Sales & Technical Support
🔧 Common Problems
Possible operating symptoms include interruptions in cartridge feeding, uneven presentation in the rotary positioning parts, or cartridges hesitating during transfer. Filled quantities may vary, visible bubbles may appear in the liquid, or droplets may remain at the filling outlet. Rubber piston stoppers may arrive inconsistently, sit at an angle, or finish at different positions within the cartridges. Residual air between the liquid and stopper may vary between samples. The no-stopper alarm may recur during operation. Other symptoms include irregular pneumatic movement, abnormal indexing noise, incomplete cartridge ejection, or accumulation at the finished-product conveyor. Product leakage may be visible around accessible tubing connections or the filling outlet.
🛠 Troubleshooting
Problem: Cartridges hesitate or enter the rotary assembly unevenly. Possible Cause: Misaligned guides, debris, or packaging that differs from the approved samples. Recommended Solution: Stop the machine and inspect the affected presentation area before reviewing the guide setup.Problem: Filled quantity varies during production. Possible Cause: Incorrect tubing installation, air entering the pathway, or changing product condition. Recommended Solution: Inspect the pathway and liquid supply before repeating the agreed dose test with representative material.Problem: Product drips after filling. Possible Cause: Residue at the outlet, unsuitable shut-off timing, or wear in the nozzle assembly. Recommended Solution: Clean and inspect the outlet before checking the shut-off sequence under the approved setup procedure.Problem: Piston stoppers finish at inconsistent positions. Possible Cause: Irregular stopper presentation, mismatched components, or an unsuitable insertion setting. Recommended Solution: Inspect the complete package and stopper feed before reviewing insertion adjustments.Problem: Residual air varies after stoppering. Possible Cause: Inconsistent vacuum conditions, entrained air in the liquid, or variation in package presentation. Recommended Solution: Assess incoming product condition and stoppering operation separately before changing the process settings.Problem: The no-stopper alarm repeats or output transfer is interrupted. Possible Cause: Insufficient stopper supply, feed-path obstruction, or restricted finished-cartridge movement. Recommended Solution: Inspect the relevant supply or discharge path after safe isolation before adjusting or replacing components.
🧼 Cleaning Method
1. Stop the machine according to the operating procedure. 2. Remove remaining cartridges and stoppers from the processing area. 3. Recover residual liquid using the established product-handling procedure. 4. Isolate the electrical supply under the maintenance instructions. 5. Isolate compressed air and vacuum services according to the equipment procedure. 6. Relieve retained pressure or vacuum before accessing affected components. 7. Remove accessible product-contact parts according to the machine instructions. 8. Clean reusable product-path components using a compatible approved method. 9. Replace tubing designated for single-use service under the production procedure. 10. Clean accessible filling-nozzle components according to their service instructions. 11. Clean cartridge-positioning parts and stopper guides with suitable non-damaging materials. 12. Wipe enclosure and external surfaces without flooding electrical components. 13. Inspect cleaned parts for retained product, particles, or cleaning residues. 14. Dry reusable components using the established production procedure. 15. Perform any required sanitization under the facility’s approved method. 16. Reassemble removed parts according to the equipment instructions. 17. Record cleaning completion according to the facility’s documentation requirements.
📋 Maintenance
1. Inspect peristaltic tubing for flattening, cracking, leakage, or visible deterioration. 2. Examine product-path connections for loosening or damage. 3. Check the filling outlet for buildup or irregular shut-off movement. 4. Inspect cartridge guides and positioning parts for wear affecting support. 5. Examine stopper feed guides for residue, damage, or loose fittings. 6. Check stopper insertion tooling for visible wear or misalignment. 7. Inspect accessible vacuum connections for deterioration or leakage. 8. Examine pneumatic tubing and fittings for abrasion or loose connections. 9. Inspect photoelectric sensing surfaces for contamination or displacement. 10. Check the finished-product conveyor for obstruction or abnormal tracking. 11. Inspect accessible fasteners and the frame securing arrangement. 12. Keep motor and drive ventilation areas clear of accumulated material. 13. Review electrical connections through qualified maintenance personnel. 14. Apply lubrication only where specified in the installed component instructions. 15. Verify alarm operation under the prescribed maintenance check. 16. Check filling and stoppering performance after relevant maintenance. 17. Record inspections, adjustments, and replaced components in the maintenance log.
⚙️ Installation
1. Position the machine on a firm, level floor. 2. Establish access for component replenishment, enclosure opening, and servicing. 3. Secure the mobile frame according to the installation instructions. 4. Inspect cartridge-handling and stoppering components for transport damage. 5. Connect protective earthing through qualified electrical personnel. 6. Connect the electrical supply specified for the ordered configuration. 7. Connect compressed air within the required 0.4–0.8 MPa range. 8. Complete vacuum-station utility connections according to the final installation drawings. 9. Fit handling parts matched to the approved cartridge. 10. Install stopper presentation and insertion components matched to the selected piston stopper. 11. Assemble the peristaltic pathway according to the pump instructions. 12. Check component feeding under the commissioning procedure. 13. Adjust the dose using representative formulation. 14. Verify filled quantity against the agreed measurement method. 15. Assess stopper position and residual air using the approved package. 16. Check finished-cartridge transfer onto the included conveyor. 17. Document the accepted setup before routine production.
🔩 Spare Parts
Why Choose This Machine
- Aligned with preclosed cartridge packaging: The processing sequence matches cartridges filled through the piston end, avoiding the inclusion of a crimping operation that belongs to a different package-preparation stage.
- Reduced transfers between operations: Feeding, dosing, vacuum stoppering, and ejection share one coordinated arrangement, limiting manual movement between individual processing stations.
- Focused residual-air management: Vacuum is applied during piston-stopper insertion, addressing the space between the filled liquid and stopper as part of closure assembly.
- Batch replenishment of components: Cartridge hopper and vibratory stopper feeding shift the operator’s task toward replenishment and supervision rather than individual component placement.
- Defined downstream handoff: The included conveyor provides a discharge route that can be considered alongside collection, inspection, and secondary packaging.
- Product-path selection: The peristaltic arrangement allows tubing compatibility and handling requirements to be assessed as part of the formulation-specific filling setup.
- Centralized operating interface: Siemens PLC and touchscreen controls bring routine machine operation to one location, supporting setup and production supervision.
Frequently Asked Questions
Installation Requirements
Provide an electrical supply matched to the ordered voltage, frequency, and phase configuration. The listed total power is 3.5 kW. Electrical connection and protective earthing must follow the machine wiring requirements and applicable installation rules.
Provide compressed air at 0.4–0.8 MPa with quality appropriate to the installed pneumatic components. Confirm the vacuum stoppering arrangement’s utility connections against the final equipment specification; a separate vacuum-source requirement is not defined here.
Route the liquid supply pathway without kinks or interference with moving components. Establish suitable storage and presentation of preclosed cartridges and rubber piston stoppers.
The surrounding environment, component preparation, and product-handling procedures must suit the intended manufacturing process. Define any required environmental controls and documentation before installation.
Related Articles


Technical Buyer's Handbook & Deep Insight
Ready to Get a Quote?
Contact our team directly for pricing, customization options, and delivery timelines.
💬 WhatsApp Us NowGet Your Download Link
Please fill in your details and we'll send the download link to your email.